Blog
Saree Making Process: How Sarees Are Made, from Yarn Preparation to Finishing

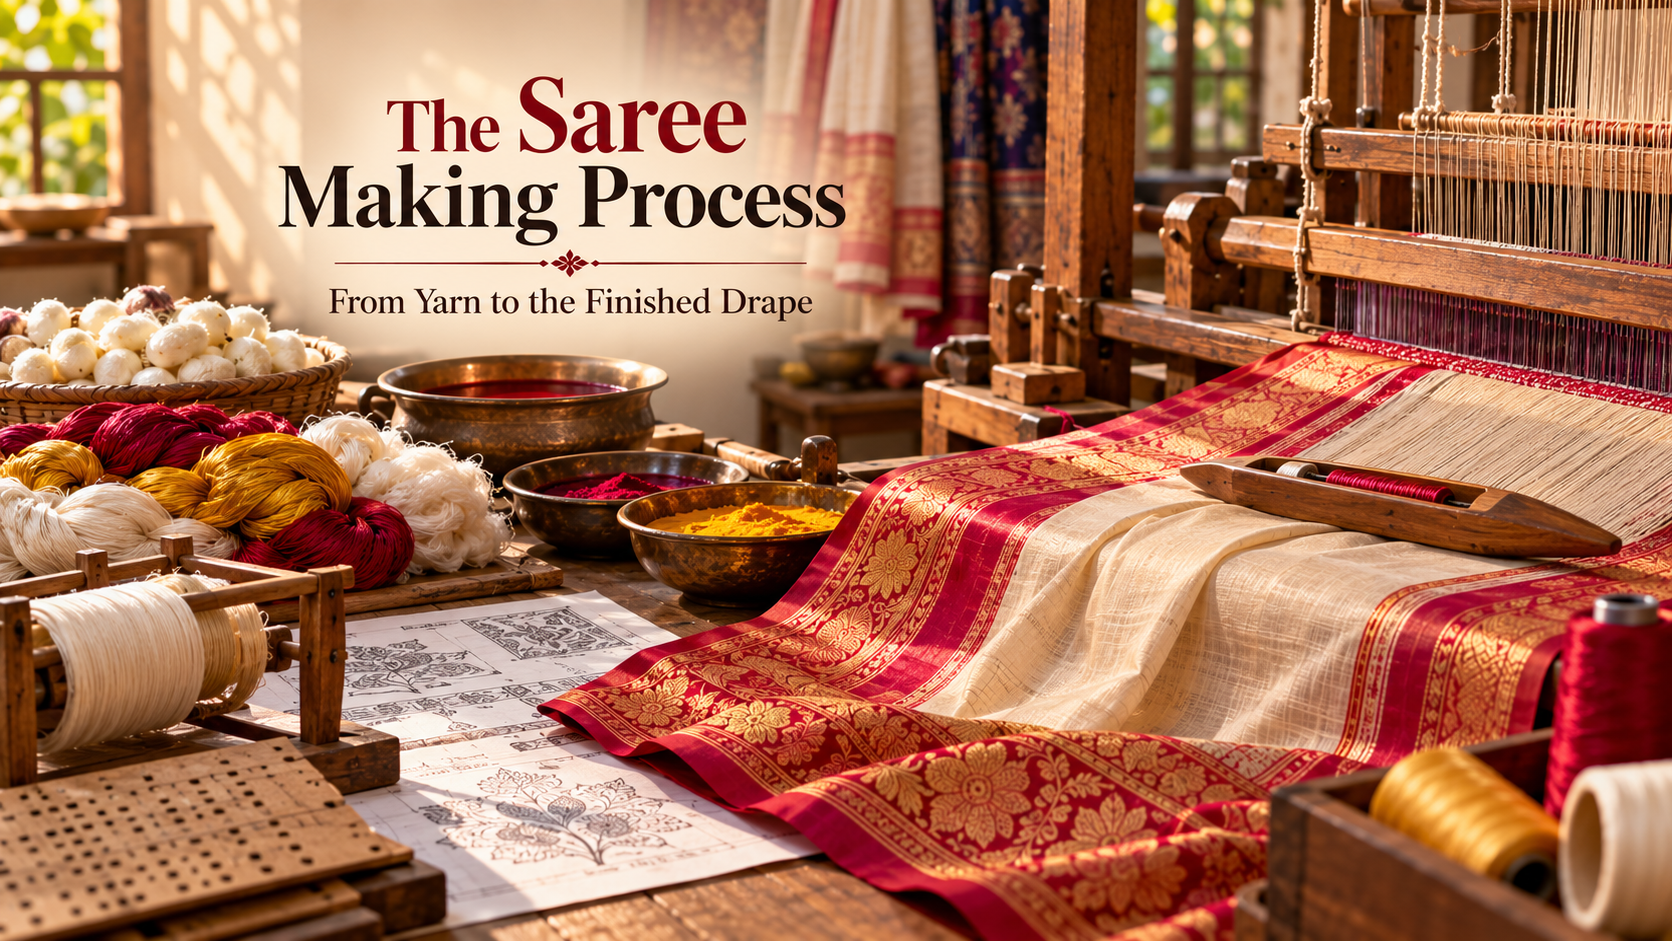
A saree looks like one long piece of cloth, and in a way it is. Most are woven as a single length of roughly 5 to 6.5 metres. What a finished saree hides is the work on either side of the loom: yarn that was boiled, dyed and wound, thousands of warp threads that were measured, stiffened and threaded one at a time, and a design that existed as a drawing or a stack of punched cards before any cloth did. The saree making process can take days to set up and, depending on the design, anywhere from a couple of days to a week or more to weave.
This guide explains how sarees are made stage by stage: yarn selection and preparation, dyeing, winding, warping, sizing, loom setup, motif creation, weaving, finishing, inspection and packaging. It also shows where the steps change for cotton, silk, ikat, jamdani and Baluchari, and where handloom and powerloom production differ at each stage. It is a production explainer, not a buying guide. If you are choosing between handloom and powerloom sarees, the site’s separate guides on handloom vs powerloom sarees and on how to identify handloom and powerloom sarees cover that question.
The saree making process at a glance
Textile researchers often split cloth production into three phases. Pre-loom work covers dyeing, winding, warping and sizing the yarn. The loom stage is weaving itself. Post-loom work covers finishing steps such as washing, bleaching, calendering or printing, depending on the product. Handloom and powerloom sarees both follow this arc, though the tools, the speed and the number of people involved differ.
Not every saree passes through every step below. A saree woven from ready-dyed synthetic yarn skips the dye house, and an ikat saree adds a tying step that others never need.
| Stage | What happens | Purpose | Output |
| 1. Fibre and yarn selection | Cotton, silk, zari, or man-made filament yarn is chosen for body, border and pallu | Fixes the cloth’s weight, texture and the way it takes dye | Yarn in hanks, skeins or cones |
| 2. Yarn preparation | Cotton is scoured or boiled; silk is degummed | Removes oils, impurities or silk gum so the yarn takes dye evenly | Clean yarn ready for dyeing |
| 3. Dyeing | Yarn is dyed in hanks, or tied and dyed in stages for ikat | Puts colour into the thread before weaving | Dyed, dried hanks |
| 4. Winding | Yarn moves from hanks to bobbins, spools or cones; weft goes onto pirns where shuttles are used | Makes the yarn run smoothly and clears faults | Warp and weft packages |
| 5. Warping | Warp threads are measured to length, counted and set in colour order | Fixes the saree’s length, width and warp-way stripes | Warp sheet or beam |
| 6. Sizing and dressing | A starch-based size is applied to the warp, which is then dried and wound on the beam | Reduces friction and breakage during weaving | Sized warp on the weaver’s beam |
| 7. Loom setup | Each warp end is drawn through a heald and a reed dent, then tied to the cloth beam | Controls which threads lift and how closely they sit | A loom ready to weave |
| 8. Design and motif preparation | The design is drawn on graph paper and turned into dobby settings, jacquard cards, jala patterns or extra-weft plans | Converts a drawing into instructions the loom can follow | Pattern cards or a loom set for the design |
| 9. Weaving | The loom lifts warp threads, passes the weft and presses it into place | Interlaces warp and weft into cloth | A woven saree length |
| 10. Cutting and finishing | The cloth is cut from the loom, loose threads are trimmed, and washing, finishing and pressing follow as the tradition requires | Cleans the cloth and settles its texture | A finished saree length |
| 11. Inspection and mending | The cloth is checked for faults, which are repaired or rewoven | Catches weaving flaws before sale | An approved saree |
| 12. Folding and packaging | The saree is folded in the style of its tradition, labelled and packed | Protects the cloth in transit | A packed saree |
Stage 1: Choosing fibre and yarn
The first decision is the fibre. Cotton, silk and man-made filament yarns behave differently on the loom and in the dye bath, and a single saree often mixes them: a cotton body with a zari or art silk border, for example. The GI specification for the Dhaniakhali saree of Hooghly describes 80s to 100s cotton yarn for warp and weft, with artificial zari or art silk used for border designs.
Yarn thickness is described by count. In the cotton count system, a higher number means a finer yarn, so 100s cotton is finer than 40s. Silk has its own grading. The GI application for Garad cites 90 to 92s silk yarn, and the GI description of Korial mentions 100-count mulberry silk.
The weaver often does not make the yarn. The Korial description notes that weavers buy silk and zari from local supply shops, and that the mulberry silk comes from cocoons reared by farmers, with some imported from South India by traders. Mills producing sarees at scale also work with synthetic filament yarns such as nylon and polyester, according to loom manufacturers who supply saree weaving units.
Stage 2: Preparing the yarn before dyeing
Raw yarn is not ready for the dye bath, and the preparation depends on the fibre.
Cotton yarn
Spun cotton arrives in hanks, which are loose loops of yarn, and it still carries natural oils and impurities. In Venkatagiri, Andhra Pradesh, the hanks are boiled to remove impurities, soaked overnight and rinsed before dyeing. Other accounts describe scouring, which is washing or boiling to take out oils and dirt, followed by bleaching and drying in the sun.
Silk yarn
Silk begins as a single continuous filament inside a cocoon. The cocoons are heated or boiled, which kills the pupa and softens sericin, the gum that holds the filament together. The filament is then reeled off, and several filaments are twisted together into yarn in a step called throwing. Traditional silk terminology names the twisted yarn used for warp organzine and the softer yarn used for weft tram.
Wild silks differ. The Assam government’s sericulture notes say muga cocoons are cooked in an alkaline soda ash solution for about an hour before reeling, and that muga weavers often prefer untwisted yarn for weft.
Thrown silk still holds a good deal of sericin, which leaves it stiff and dull. Degumming, also called boiling off or stripping, removes it with hot water, often with soap or mild alkali. In skein dyeing, the silk is degummed first and dyed afterwards. What remains is soft, lustrous silk that takes colour well.
Stage 3: Dyeing the yarn
Most handloom sarees are woven from yarn that was dyed before weaving. The reason is practical: stripes, checks, contrast borders and coloured pallus come from arranging threads of different colours on the loom, so the colour has to be in the thread first.
Hank dyeing
Dyeing is usually done in hanks or skeins, in small lots, with natural or synthetic dyes. After dyeing, the hanks are washed and dried. Some accounts of indigo dyeing describe deep vats dug into the ground to keep the dye solution free of oxygen. Dyeing for handlooms is often done in and around weaving villages by local specialists, so the dyer is a different person from the weaver. Pre-dyed yarn is increasingly bought from dye houses or suppliers as well.
Ikat: dyeing that makes the pattern
Ikat changes the usual order of design and weaving. The pattern is made in the dye bath. Following a design drawn on graph paper, artisans bind sections of yarn tightly with waterproof material, so the bound parts resist dye. The bundles are dipped, untied, retied in new places and dyed again for each additional colour. When the threads reach the loom, the pattern is already inside them. In single ikat only the warp or the weft is patterned. In double ikat both are, and the weaver must align them exactly. The slight shifting of threads during weaving gives ikat its soft, feathery edges. The site’s article on the Pochampally ikat saree shows how this shapes a finished saree.
Yarn-dyed and piece-dyed production
Some mill production works the other way round. It weaves undyed “grey” cloth and dyes or prints the whole piece afterwards. Weaving-mill process charts show both a yarn-dyed route, where yarn is dyed before it is wound for weaving, and a solid-dyed route.
Stage 4: Winding
Winding moves yarn from one package to another so that it runs cleanly through the next process. It also gives a chance to catch yarn faults. Hanks cannot go straight onto a loom because they are loose loops. They are wound onto bobbins, spools or cones first.
In weaving households, bobbin winding is commonly done by women of the family, using a charkha or a bobbin winder. Mills use cone winding machines. The weft yarn needs its own preparation. On shuttle looms, weft is wound onto pirns, which are small spools that sit inside the shuttle. Shuttleless looms such as air-jet, water-jet and rapier machines take weft from larger packages, so they skip pirn winding.
Stage 5: Warping
The warp is the set of threads that runs the length of the saree. Warping decides how long the cloth will be, how many threads it has and in what order the colours fall. On a handloom, yarn is wound around a drum or pegs, and the weaver’s plan sets the dimensions. The drums help count the threads and group them by colour. The warp is then transferred as a whole onto the weaver’s beam, a large roller.
A warp is often prepared long enough for several sarees. One account of a handloom cluster describes a warp of about 34 metres for five sarees. In mills, sectional warping machines wind equal lengths of yarn in sections onto a drum and then onto the beam.
For ikat, an extra step comes first. The yarn is wound on a frame to the required length before it is tied and dyed, so the tied sections line up with the pattern.
Stage 6: Sizing and dressing the warp
Warp threads rub against the reed and healds thousands of times while weaving, and fine yarn can fray or snap. Sizing coats the warp with a starch-based paste to strengthen and lubricate it. In weaving-industry terms, sizing improves the yarn’s smoothness and elasticity and reduces friction and static.
On a handloom, the warp is stretched out, usually in the open, and the size is brushed on. One handloom maker describes a thin, rice-based size on silk warp. A weaving-training document for handloom units describes sizing hanks in a tank, squeezing them evenly and drying them. In a mill, a sizing machine does the same job at speed. Dressing then prepares the dried warp and winds it onto the beam.
Stage 7: Setting up the loom
Loom setup is the slowest preparation step and one of the least visible. Each warp thread must be placed in exactly the right position, and a mistake here can spoil the whole weave. Retail accounts of silk saree making say setup takes hours and sometimes days.
Drafting and denting
Drafting means choosing which heald frame, or harness, controls each warp thread, based on the design. A heald is a cord or wire loop with an eye that guides a single thread, and lifting a heald lifts its thread. Denting then draws the warp ends through the gaps in the reed, a comb-like frame. One, two or more ends can go through each gap, as the weave plan requires.
Denting affects the cloth’s look. Shantipur weavers deliberately pass several threads through each gap in the reed, which leaves a faint tube-like mark in the cloth, and they choose to keep it, according to the GI application for the Shantipuri saree.
Tying in and tying up
When a loom already holds a warp that is nearly finished, the new warp can be tied to the old one instead of redrawn end by end. Mills use this shortcut often. Then the loom is gaited up and tied up, which means its treadles, or its dobby or jacquard, are linked to the healds so the correct threads lift for each row.
The loom itself
Handloom saree weaving commonly uses a pit loom, where the weaver’s treadles sit in a pit under the loom, or a frame loom, which has a raised frame. The Dhaniakhali specification names fly-shuttle pit looms, and the Mangalagiri sarees of Andhra Pradesh are woven only on pit looms. Mills use powerlooms, from plain mechanical looms to automatic and shuttleless machines.
Stage 8: Creating motifs and patterns
A saree’s design begins long before weaving. In many clusters, a designer or master weaver draws the pattern on graph paper, where each square stands for a thread position. Weavers refer to a design as a naksha, and the Dhaniakhali specification refers to naksha par, a border with an extra-warp design. How the drawing becomes cloth depends on the technique.
- Dobby. A dobby attachment lifts chosen warp threads in a set order, suited to small, repeated, geometric designs, often in borders. In Shantipur, a barrel dobby arrived in the early 1920s. Dhaniakhali weavers adopted a six-lever barrel dobby in the early 1940s, and lattice dobbies now handle larger designs.
- Jacquard. A jacquard controls warp threads individually, so it can weave large figured designs. Baluchari is the classic example: the design is drawn on graph paper, coloured, and punched onto cards that are laced together in order and fixed to the jacquard machine. In Shantipur, the weaver Devendranath Mukhopadhyay introduced the jacquard.
- Jala. This hook-like device is used on traditional Bengal looms to build motifs such as butis. The Korial description says jala designs form the pallu and the small motifs on the ground.
- Extra weft by hand. In jamdani, motifs are added one at a time by hand using a supplementary weft. Two weavers often sit side by side at the loom, interlacing each motif’s threads with fine bamboo sticks and separate small spools.
- Zari and extra threads. Zari is metallic or metal-look thread. It is woven in as extra warp or extra weft, and the Korial and Dhaniakhali descriptions note that the zari used is mainly artificial.
Powerloom mills use dobby and jacquard machines too. Loom makers market both for saree borders and pallus, including electronically controlled jacquards.
Stage 9: Weaving
Once the loom is set and the design is loaded, the cloth can be woven. Every loom, whether hand-operated or electric, repeats the same sequence of motions:
- Shedding. Warp threads are lifted to open a gap called the shed.
- Picking. The weft is passed through the shed, either by a shuttle or by another weft-carrying device. One pass is called a pick.
- Beating up. The reed presses the new weft against the cloth already woven.
Two further motions support these. Let-off releases warp from the warp beam, and take-up winds the finished cloth onto the cloth beam.
On a handloom
The weaver lifts groups of warp threads with foot treadles, sends the shuttle across, and beats each pick into place. A fly shuttle is sent across by pulling a cord, which is faster than throwing it by hand. The weaver controls tension through feel, which is why small variations are part of handwork. Weaving time depends heavily on the design. A Baluchari saree takes about five to six days with two weavers working in shifts once the jacquard is set. The Dhaniakhali listing from the West Bengal handloom body says a saree can take between two and five days. Jamdani is described as one of the most time-consuming handloom techniques, because every motif is added separately by hand.
On a powerloom
A powerloom does the same motions automatically, at much higher speed. Indian powerlooms range widely: plain looms without automatic stop motions, semi-automatic and automatic looms, and shuttleless machines that insert weft with a jet of air or water or with mechanical rapiers. An air-jet loom can insert 800 to 1,000 picks a minute, according to a weaving-industry overview. Many powerlooms are fitted with dobby or jacquard heads, so a machine can weave borders and pallus too.
Stage 10: Cutting off the loom and finishing
When the length is complete, the weaver cuts it from the loom. Several finishing steps follow, and they vary by tradition.
- Trimming. Loose threads are removed. Where extra weft floats between motifs, as in the cutwork technique used in some Banaras brocades, the unwanted floats are clipped with scissors after weaving.
- Washing and settling. Some workshops wash the cloth to remove size, then stretch, dry and press it to bring out its texture and sheen.
- Tradition-specific finishing. The GI applications for Garad and Korial describe a traditional khai finish, followed by folding into a special shape called pat. Baluchari is polished after weaving.
- Mill finishing. Post-loom processing in mill production can include bleaching, anti-shrink treatment, printing and calendering, which is pressing the cloth between rollers.
Some sarees receive extra work from different people after weaving, such as embroidery or printing.
Stage 11: Inspection and mending
Inspection happens during weaving as well as after. Weavers watch for broken threads and uneven picks as they work, and a section sometimes has to be redone. In clusters such as Venkatagiri and Mangalagiri, the master weaver inspects finished sarees to rectify flaws. In mills, grey cloth is inspected after weaving and sent to a mending section before folding. This is quality control inside the workshop. It is a different matter from the checks a buyer might make, which the site’s guide on how to identify a good-quality saree covers.
Stage 12: Folding and packaging
Folding is part of the tradition in some clusters. Shantipur sarees are marketed in a traditional fold called guti bhanj, and Garad sarees are folded into the pat shape. After folding, the saree is labelled and packed to travel. The labels and documents a handloom saree might carry, such as the Handloom Mark, are explained in the identification guide above.
Who does what: the people behind a saree
A finished saree passes through many hands. The division of labour differs from one cluster to another.
| Role | Work | Stage |
| Sericulture farmers, reelers and spinners | Rear cocoons and reel silk, or spin cotton | Stage 1 and 2 |
| Dyers | Scour and dye yarn, often in or near the weaving village | Stage 2 and 3 |
| Winders | Wind yarn onto bobbins and pirns; often household members on handloom, machine operators in mills | Stage 4 |
| Warpers and sizers | Measure, set and strengthen the warp | Stage 5 and 6 |
| Designers and card punchers | Draw the naksha and prepare dobby settings or jacquard cards | Stage 8 |
| Weavers and assistants | Set up the loom and weave; jamdani and Baluchari often use two weavers | Stage 7 and 9 |
| Finishers and menders | Trim, wash, press, repair and fold | Stage 10 to 12 |
| Master weavers and cooperatives | Coordinate yarn, designs and weaving, and inspect the finished cloth | Across stages |
Two accounts show how much the arrangement varies. For Korial sarees, the weaver family has historically handled every step from preparing yarn to final weaving. For tant, a photo documentary of the Bengal cluster describes yarn processing, colouring, dyeing, drying, designing, weaving and marketing as work done by separate groups in a locality.
How the saree making process changes by fabric and tradition
| Fabric or tradition | What changes | Stage affected |
| Cotton tant (Shantipur, Dhaniakhali) | Fine cotton yarn on fly-shuttle pit or frame looms; dobby borders; some hand-added butis; reed marks in Shantipur | 1, 7, 8 |
| Silk (Garad, Korial) | Silk is degummed; fine two-ply yarn; jala patterns; khai finish and pat fold | 2, 8, 10 |
| Ikat | Tying and dyeing set the pattern before weaving | 3, 7 |
| Jamdani | Extra weft added by hand, motif by motif, often by two weavers | 8, 9 |
| Baluchari | Design cards punched for a jacquard loom | 8, 9 |
| Mill or powerloom production | Cone winding, sectional warping, sizing machines, shuttleless looms, grey inspection | 4 to 11 |
| Synthetic filament sarees | Yarn arrives ready-dyed and needs no scouring or degumming | 2, 3 |
Handloom and powerloom: stage by stage
The differences between handloom and powerloom sarees show up at particular stages. Many early stages match: the yarn still has to be chosen, dyed, wound, warped and sized. The table lists typical practice at each stage. “Powerloom” covers a wide range of equipment, so a given unit may differ.
| Stage | Typical handloom practice | Typical powerloom or mill practice |
| Winding | Charkha or bobbin winder, often by household members | Cone winding machines; pirn winding only for shuttle looms |
| Warping | Drum or peg warping by hand | Sectional warping machines |
| Sizing | Size brushed on stretched hanks or warp | Sizing machines |
| Drawing-in | Done by hand end by end, or by tying in | Manual or semi-automatic; automatic drawing-in and knotting machines exist |
| Weaving | Hand and foot operated; weaver controls tension | Automatic motions at higher speed; shuttle or shuttleless |
| Inspection and mending | Weaver or master weaver | Grey inspection, then a mending section |
For what these differences mean to a buyer, see the guides linked in the introduction. This article only follows the production steps.
Textile terms in plain language
| Term | Meaning |
| Hank | A loose loop of yarn wound for dyeing and washing |
| Yarn count | A number for yarn thickness; in the cotton system a higher count means a finer yarn |
| Scouring | Washing or boiling to remove oils and impurities |
| Sericin | The gum that binds silk filaments in the cocoon |
| Degumming | Removing sericin so silk becomes soft and lustrous |
| Warp | The lengthwise threads held on the loom |
| Weft | The crosswise thread carried through the warp |
| Pirn | A small spool of weft yarn that sits inside a shuttle |
| Beam | A large roller that holds the warp or the finished cloth |
| Sizing | Coating the warp with starch to strengthen it for weaving |
| Heald | A loop with an eye that guides one warp thread and lifts it |
| Reed and dent | A comb-like frame that spaces the warp; each gap is a dent |
| Shed | The gap made when some warp threads lift |
| Pick | One pass of weft through the shed |
| Selvedge | The self-finished edge of the cloth |
| Grey cloth | Cloth straight off the loom, before finishing |
| Dobby | A loom attachment for small, repeated, geometric patterns |
| Jacquard | A mechanism that controls warp threads individually for large figured designs |
| Jala | A hook-like pattern device used on traditional Bengal looms |
| Extra (supplementary) weft | Added weft used only where a motif is wanted |
| Zari | Metallic or metal-look thread used in borders and motifs |
| Anchal or pallu | The decorated end piece of the saree |
| Khai finish | A traditional finish used on Garad and Korial sarees |
Where Mahavir Cloth Center fits
Mahavir Cloth Center is a clothing store in Shirol, Kolhapur, Maharashtra, and its website lists sarees, kurta suits, kids’ clothing and hosiery. Its blog covers what to look for in a saree, and this article adds the production steps behind the cloth. It describes general methods and does not describe how any particular saree in the store was made. Readers who want to see what is currently available can browse the saree collection.
FAQs
How is a saree made step by step?
The steps are choosing and preparing yarn, dyeing, winding, warping, sizing, setting up the loom, preparing the design, weaving, finishing, inspection and packaging. Not every saree uses every step. A saree made from ready-dyed yarn skips dyeing, and an ikat saree adds a tying stage.
How long does it take to weave a saree?
It depends on the design and loom. Once the jacquard is set, a Baluchari saree takes about five to six days with two weavers working in shifts. A Dhaniakhali saree can take two to five days. Jamdani is slower because each motif is added by hand. Preparation before weaving adds time on top of this.
What is the difference between warp and weft?
The warp is the set of lengthwise threads held under tension on the loom, and the weft is the crosswise thread that passes through them. Weaving is the interlacing of the two. Borders and stripes in the warp direction are set at the warping stage.
Why is yarn dyed before weaving?
Many sarees get their colour pattern from coloured threads, such as stripes, checks, contrast borders and coloured pallus. Dyeing the yarn first puts the colour where the loom needs it. Mills sometimes weave grey cloth and dye or print the whole piece afterwards.
What is sizing, and why is it done?
Sizing is coating the warp threads with a starch-based paste. It strengthens and lubricates the yarn so it does not fray or break against the reed and healds during weaving. Workshops may wash the cloth afterwards, and how much size remains depends on the fabric and the finishing.
What do dobby and jacquard do?
Both are shedding mechanisms that decide which warp threads lift for each pick. A dobby suits small, repeating geometric patterns, usually in borders. A jacquard controls threads individually, which allows large figured designs such as a Baluchari pallu.
Do handloom and powerloom sarees go through the same stages?
They share the same broad sequence of yarn preparation, warping, sizing, weaving and finishing. They differ in how each stage is done. Powerloom units use machines for winding, warping, sizing and weaving, and handloom units rely on hand and foot operation for most of these.
Conclusion
Seen as a sequence, the saree making process explains many of the details people notice in a finished saree. Stripes and borders come from how the warp was warped and dyed. A fine, even surface starts with sizing and careful winding. A figured pallu begins as a drawing and a set of punched cards. The soft sheen of silk exists because someone removed its gum, and a faint reed mark in a Shantipur saree comes from how threads were drawn through the reed.
None of these steps is visible on its own, but each leaves a trace in the cloth, and each is done by a different set of people. Knowing the stages gives you better words for what you are looking at, whether the saree is a cotton tant, a Garad silk, an ikat or a mill-woven piece. That vocabulary is the basis of informed appreciation, and it makes it easier to ask a seller or weaver specific questions.